UX Design & Research · NDA · Enterprise MES · 1 Designer - 3 Devs - 1 PO · 2 years
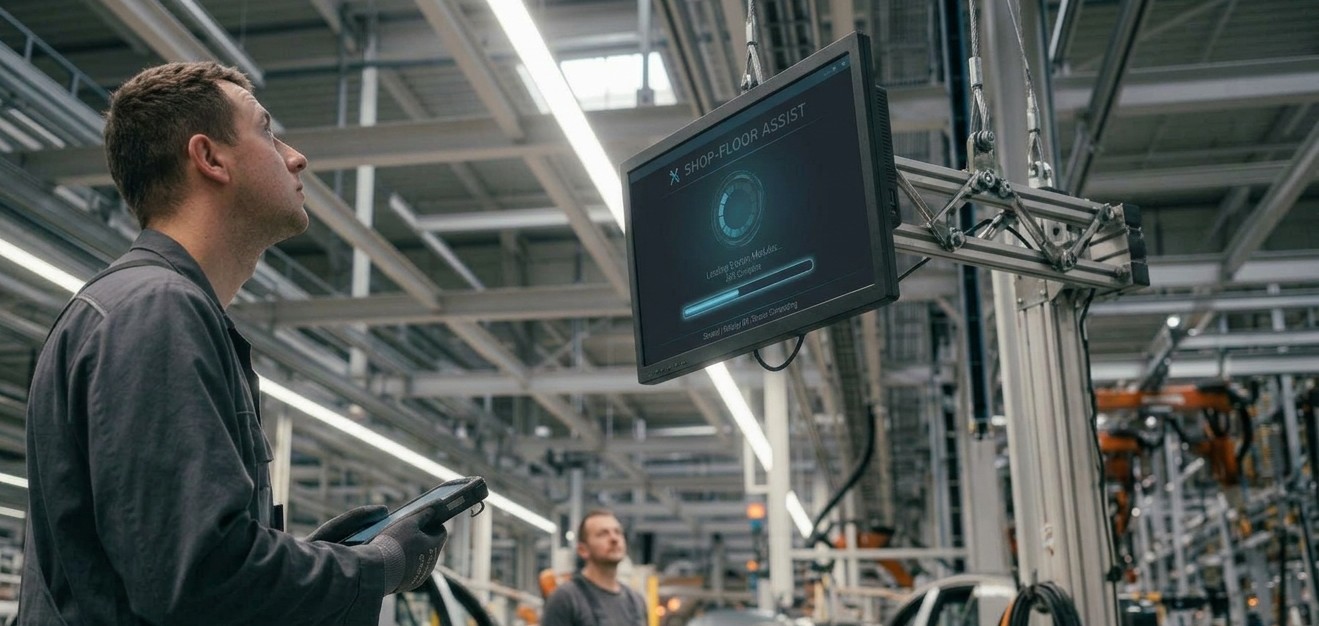
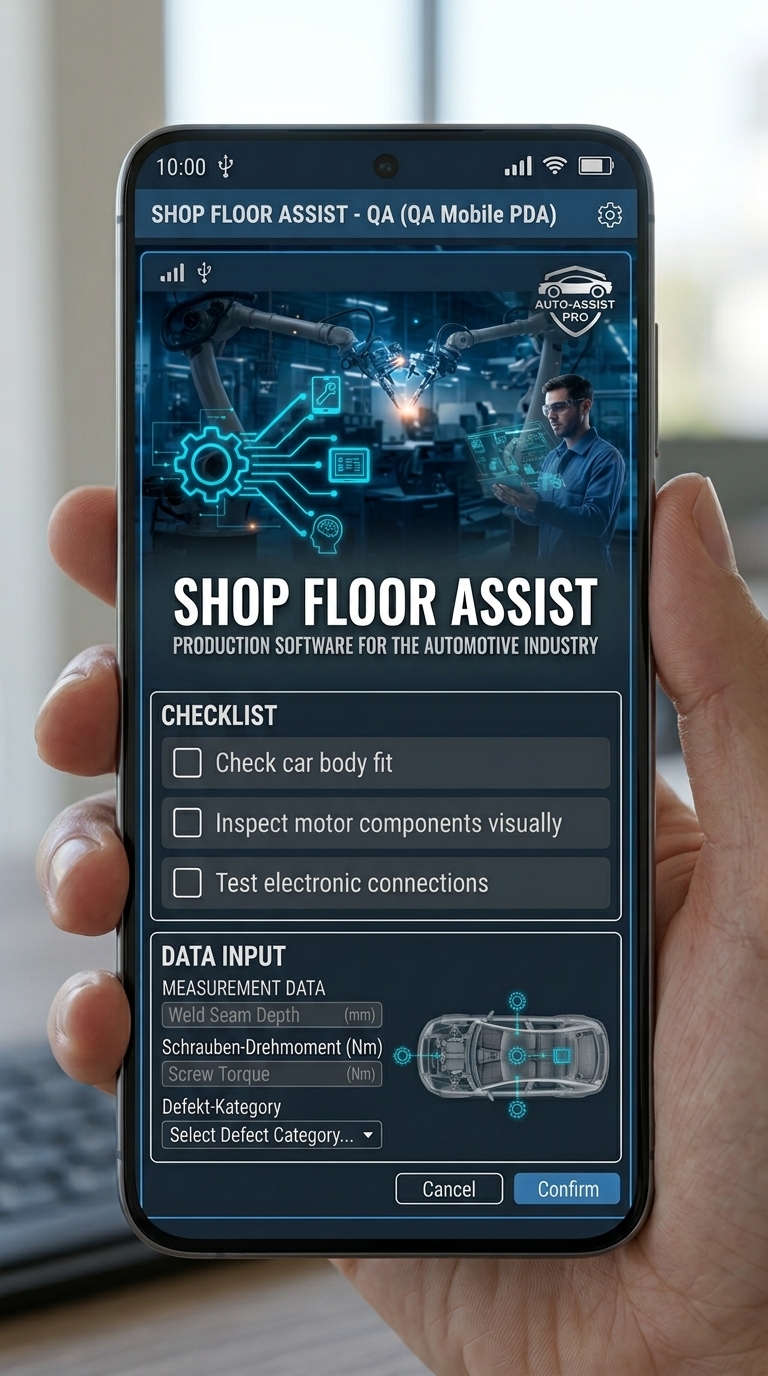
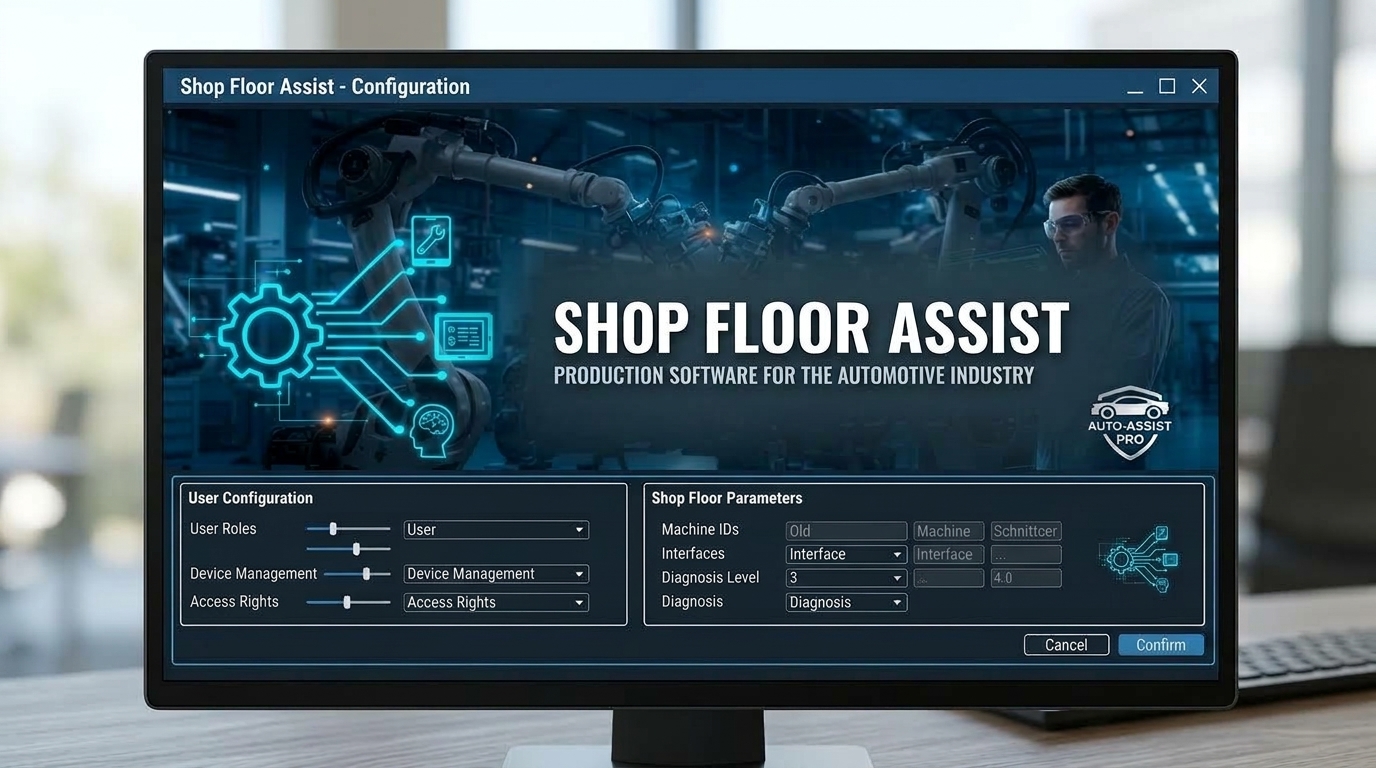
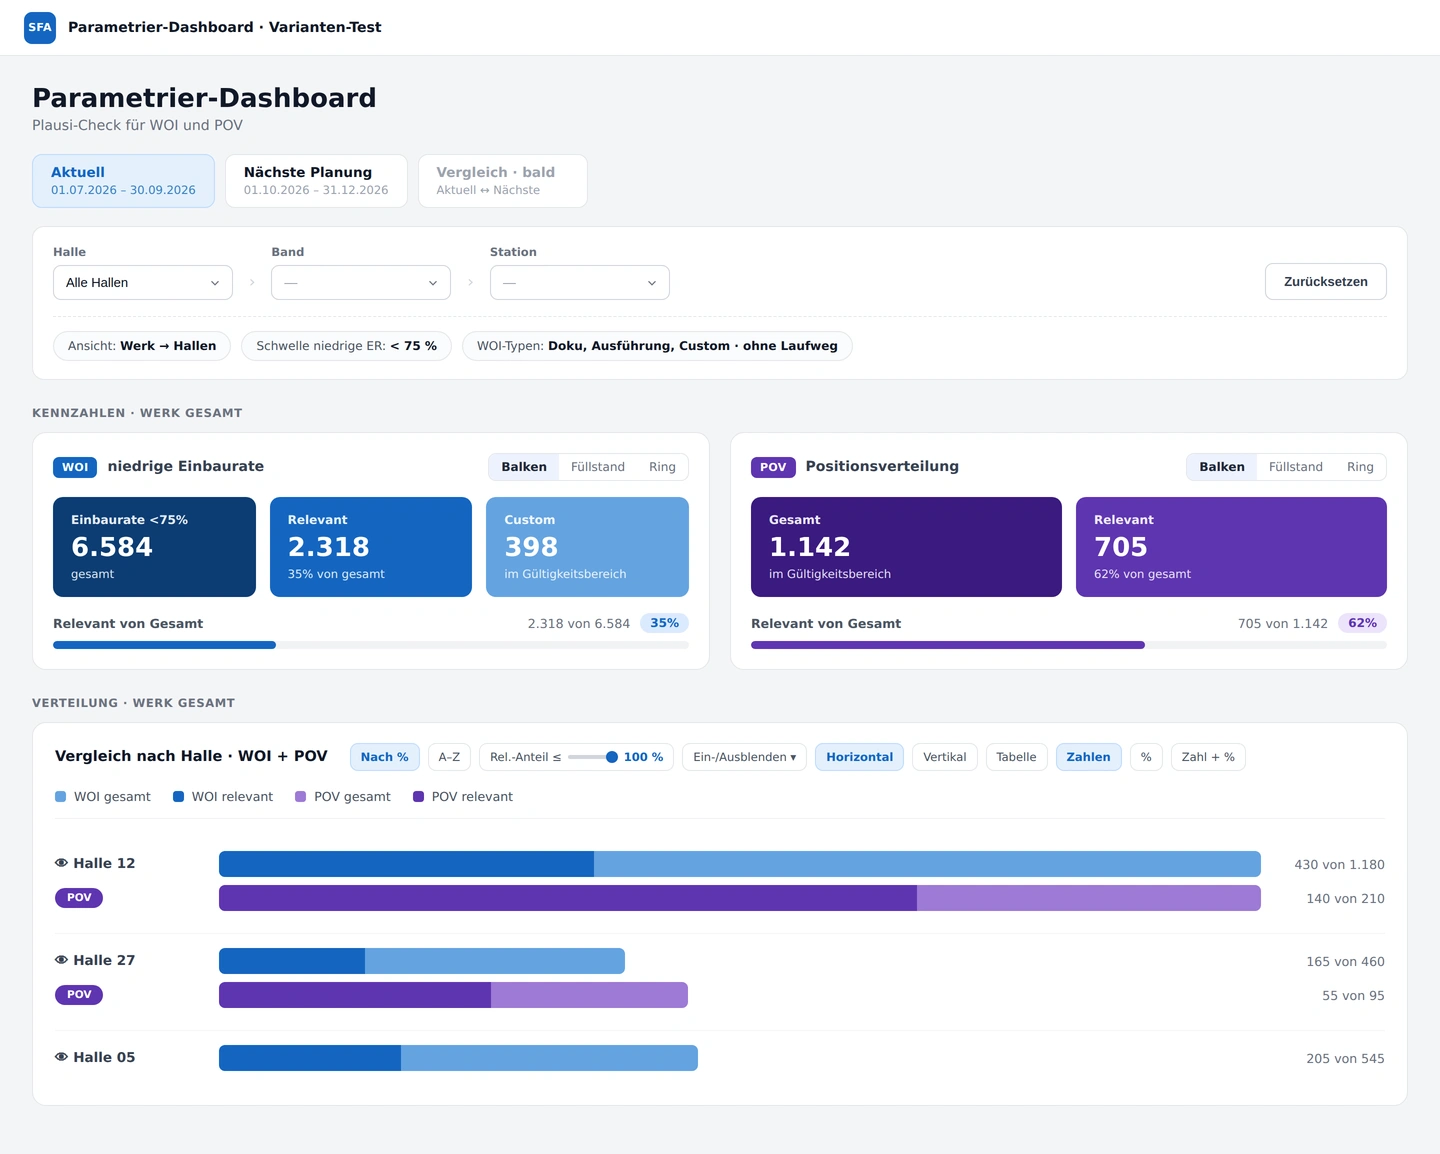
An assistance system for automotive final assembly: a high-mounted production monitor, a handheld (PDA) for inspection and special steps, a configuration dialog for parametrisation, and a dashboard for oversight. This case study focuses on the production monitor as the core — with the three adjacent parts in overview.
Assembly workers need the right build information at a glance while working to takt — in a loud hall, often wearing gloves, in front of a high-mounted monitor. But the monitor is only one part: inspection and special steps run on a handheld (PDA), the per-station content is parametrised up front in a configuration dialog, and a dashboard gives the people doing that parametrisation oversight and control. This case study covers the production monitor in depth and the three further parts in brief.
The monitor is mounted high so everyone can see it — which means only the lower half is reachable, especially for shorter workers. It's read from 1–3 m, often with gloves, in a loud hall.
And nothing may be scrolled away or paged — not for lack of space, but because the plants explicitly want it that way. Anyone working to takt on the line shouldn't interrupt their work to navigate the monitor. Everything important has to be there at a glance.
"The standard steps I do in my sleep. I just need to see instantly when something's different."— Proto persona "experienced worker" · illustrative
An experienced worker knows the motions by heart and does them almost blind. For them the monitor shouldn't show the routine but the exception — deviation, special case, special equipment — instantly and unmistakably. At the same time, the same monitor must guide new workers and working students safely, step by step. The routine recedes, the exception jumps out.
"I'm still unsure — I need every step clear and in the right order."— Proto persona "new worker / working student" · illustrative
Guide where it counts, freedom where it doesn't: the default is to inform and orient. The system only guides bindingly for takt, quality or safety — an open inspection step, an imminent line stop. In free work, the decision stays with the worker.
Contextual inquiry on the line: mounting height, reach envelope, glove use, noise, viewing distance, and the age/height/experience spread of the workforce.
Turn the environment into hard design constraints: reach zone, no-scroll, distance legibility, no forced actions.
Rescale a Material-based component library for distance and gloves instead of designing from zero; define the reach-zone layout and handheld patterns.
Self-contained, testable single-file prototypes for both surfaces; validate structure and interaction logic.
Review against distance legibility, glove hit-accuracy, overflow-without-new-space, and the "guide where it counts" principle.
Document the adapted component set, the reach-zone layout, and the handheld interaction pattern for engineering.
The display sits above head height; the top is visible but not reliably touchable.
Gloved fingertips miss small targets; swipe is unreliable; audio is lost in the hall.
There's no time to scroll during takt — everything needed has to be visible at once, on a single screen (plant requirement).
An implied automatic consequence creates unsafe obligations on a safety-relevant line.
The most important actions stay permanently anchored in the lower, reliably reachable zone. Since only the lower half of the display is safely reachable in the production environment, interaction is designed around it.
Swipe gestures proved unreliable, especially when operated with work gloves. They were replaced with clearly recognizable, oversized tap targets.
Existing library components were deliberately scaled and adapted to the demands of the production hall — especially regarding touch targets, legibility, and operability under harsh conditions.
The visually elaborate tile layout was dropped in favor of a minimalist, text-based display. On the small screen, fast legibility of relevant information takes priority.
Decorative or unnecessarily complex UI elements were deliberately avoided. Instead of modern design for its own sake, the principle holds: as simple as possible, as much as necessary — focused on a solution that is genuinely feasible and viable under the given technical and operational conditions.
Each deep dive walks through a single design challenge in detail — three as a pattern applied across several surfaces, one as a concrete cross-device flow.
Integrating new information into an already-shipped UI — best outcome, least change effort.
A pattern for work-step status, applied three times.
A new tile on an already-full screen — and a restructuring of the workstation configuration.
One shared design for two devices whose technical interplay was unclear at the outset.
Not everything happens on the monitor. Safety-relevant stamping, scan-based product-data capture and the fallback mode on device failure run on a handheld (PDA) — one-handed, in short steps, with unambiguous success/error feedback.
Screens under NDA · description [proto] based on the project documentation.
What the monitor shows per station is defined up front: in a desktop configuration dialog, a dedicated role at the customer (the parametriser) sets up workstations, operations, layouts and inspections — along a deep hierarchy (plant → hall → line → station → workstation). A business-critical enabler that decides what reaches the line.
To close, a brief look at the dashboard for the parametrisers: "What have I parametrised? Where are the anomalies? What's still open?" At scale (many halls, dozens of lines) it makes the proportions visible — deliberately neutral, with no good/bad verdict.
Data-viz concept · separable as a standalone enterprise case.
Pilot phase complete, main work done (~80/20), rollout adjustments ongoing. No quantitative adoption or error metrics claimed — [not verified] until field data exists.
The core wasn't to show more information, but the right information: for the experienced worker the routine recedes and the exception jumps out; the new worker is guided safely through the sequence by the same screen. And around the monitor, the invisible work — parametrisation, inspections, oversight — decides whether the right thing reaches the line at all.